
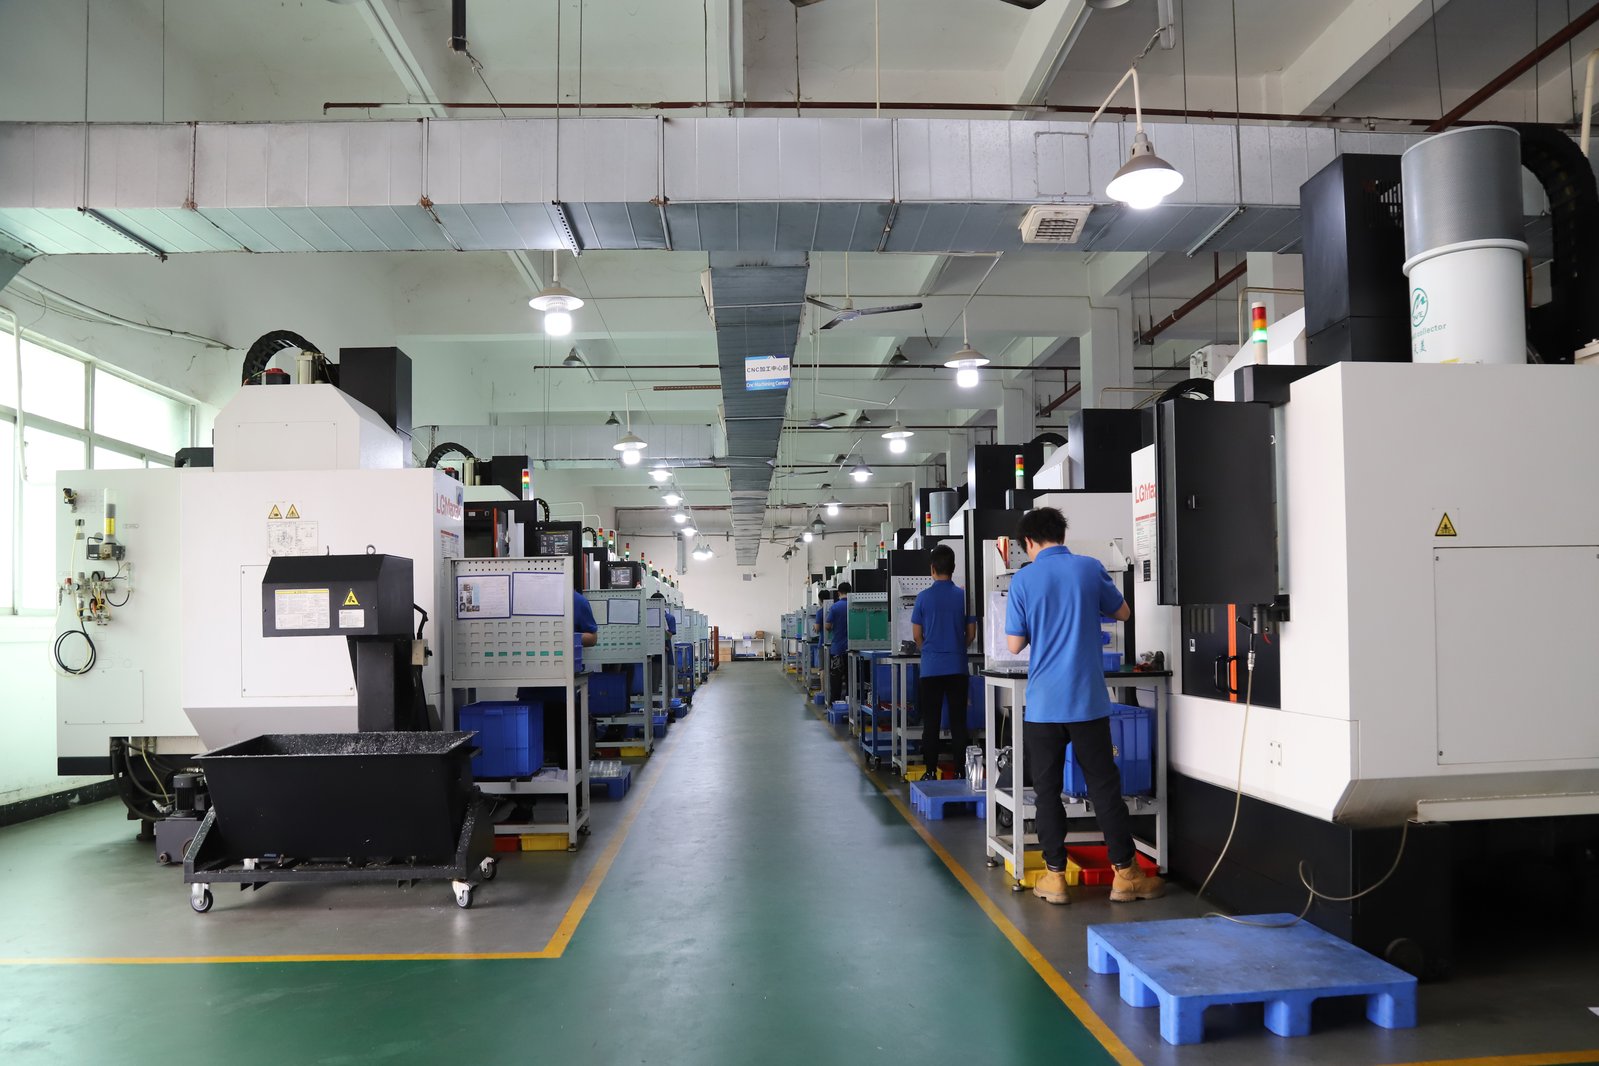
Every machining quote begins with a drawing, and every drawing is a set of numbers the factory must hold. The buyer's first question about a China machining factory is therefore not "can you machine parts?" but "what bands can you actually hold, and how do you prove it?" The honest answer is a capability table, not an adjective: milling and turning hold ±0.003 mm on controlled features, precision grinding reaches ±0.002 mm as a separate process family, and the process capability target on critical characteristics is Ppk ≥ 1.67 initial — with finishes following their own ladder from the standard machined range down to Ra 0.4 µm and below. This guide walks through the capability, the callouts, and how to specify what your part actually needs.
What tolerance bands can a China machining factory actually hold?
On a precision machining floor the dimensional capability is well defined, and it belongs on the table in numbers.
| Process family | Holds comfortably | Notes |
|---|---|---|
| Milling and turning | ±0.003 mm on controlled features | The everyday precision band on machined geometry |
| Precision grinding | ±0.002 mm | A separate process family for journals, seal diameters, and bearing seats |
| Critical characteristics | Ppk ≥ 1.67 initial | The statistical target: parts sit inside the band with margin |
| Geometric callouts | Roundness, runout, true position | Separate bands from size tolerances, verified on a CMM |
Those numbers are achievable on aerospace, medical, and automation work machined in China, and they mean nothing until the drawing defines the datum scheme and the measurement conditions. The honest capability conversation starts with the table and moves to the features your drawing actually carries, because a factory that states its bands in numbers is a factory you can audit, and one that says only "high precision" has given you nothing to verify.
Which drawing features belong on a tight band, and which do not?
The drawing is where tolerances become cost, and the discipline is to call out the band only where the function earns it. A diameter that mates a bearing, a bore that locates a shaft, a face that seals, and a journal that runs in a bushing all earn a tight band, because the function depends on them. A cosmetic surface, a non-critical step, or a general profile does not — it belongs on a general block, where the factory can cut it at the economical rate instead of routing the whole part through the precision pass.
Tolerancing only what the function needs is the cheapest single saving on a machined drawing, and it matters doubly when the part is sourced from China, where the quote is built feature by feature. A drawing that stamps ±0.003 mm on every dimension is a drawing that pays precision prices for features that never needed them. When you send a drawing to a factory, ask which callouts are driving the cost; a factory that tells you which bands to loosen is a factory reading your drawing as an engineer rather than as a rate card.
What surface finish ranges can machining actually deliver?
Surface finish follows its own ladder, with each step down costing process time and inspection.
| Finish range | How it is reached | Typical use |
|---|---|---|
| Ra 1.6–3.2 µm | Standard milling and turning passes | General machined surfaces, non-critical faces |
| Ra 0.8 µm | Refined finishing passes on the machine | Sliding fits, sealing faces, visible surfaces |
| Ra 0.4 µm | Grinding as a separate operation | Journals, seal diameters, mating precision faces |
| Ra 0.2 µm and below | Grinding, lapping, or polishing | Precision bearings, optical-adjacent seats, seal running surfaces |
Read the ladder against the function: a surface that slides or seals earns the fine finish, and a visible or cosmetic surface earns what the process leaves. The honest specification names the Ra value on the functional surfaces and leaves the rest on the standard range, because every step down the ladder is a step up the quote. A drawing that asks for Ra 0.4 µm on a surface nothing will touch is paying for grinding that the part never needed.
Why do dimensional tolerances and finishes need separate callouts?
Dimensional tolerance and surface finish are independent properties, and a drawing that blurs them will buy the wrong thing. A diameter can sit perfectly on nominal — inside a ±0.003 mm band — and still carry a rough, torn finish left by an aggressive cut; the same diameter can be mirror-smooth and out of round or eccentric to its datum. Size and texture are measured by different instruments and controlled by different process choices, which is why each needs its own callout and its own line in the quote.
The practical rule is to treat the finish callout as seriously as the tolerance callout: name the Ra value and the surface it applies to, and let the factory plan the pass. A drawing that specifies a fine finish on a functional surface without an Ra value leaves the factory to guess, and the guess decides the process, the price, and the inspection. On a sourced part, that guess is a change order waiting to happen — the finish should be on the drawing in numbers before the RFQ leaves your desk.
Texture direction belongs in the same conversation, because some surfaces function on how the finish is laid down rather than just how smooth it is. A sealing face often wants a specific lay — the direction of the surface pattern — to hold a seal or a lubricant film, and a drawing that names only Ra leaves the lay to the process. Where the function depends on the direction of the finish, say so, because the lay is controlled by the tool path and the process choice, and it is far cheaper to specify on the drawing than to discover in the test.
What geometric tolerances need their own callouts?
Size tolerances control how big a feature is; geometric tolerances control how true it is, and on a machined part the two are independent. A bore can measure the right diameter and still be out of round, off-center to its datum, or tilted, which is why roundness, concentricity, runout, and true position each carry their own callouts and their own measurement. These are the callouts that make a rotating or mating assembly work, and they are the callouts a filled-in form can hide when only size was measured.
Buyers sourcing from a China factory should name the geometric callouts explicitly and ask which instrument verifies them. True position and concentricity belong on a CMM; roundness belongs on a roundness instrument; and the report should state the measured value for each callout, not restate the drawing. A factory that measures only diameters and reports a part as conforming has verified half the drawing, and the half it skipped is the half that makes the assembly run true.
Datum discipline is the foundation under every geometric callout, because a true position or runout value means nothing without the datum scheme it is measured against. A drawing that leaves the datums implied lets every shop measure the part differently, and two factories can report the same feature as conforming and non-conforming at once. Define the datum scheme on the drawing, agree the measurement order, and confirm the report names the datum reference, because on a sourced order, the callout and the datum travel together, and the datum that is not named is the datum that will be argued about.
How is a tight tolerance or fine finish actually measured?
The tolerance story is only as good as the measurement behind it, and the measurement rules are arithmetic. An instrument should resolve about ten times finer than the band it judges, so a ±0.003 mm feature belongs on a CMM, not on a hand gauge that cannot resolve the difference, and a finish callout belongs on a surface profilometer that measures the texture rather than on a finger across the surface. Dimensional measurement references 20 °C, and a large aluminum part measured warm reads differently from the same part at the reference, which is why critical features belong in a temperature-controlled setting.
Ask the factory which instruments verify your critical features and ask to see the calibration story behind them, because a measurement claim made on an instrument that has drifted is a claim about the past. And agree the reporting up front: which features appear on the CMM report, which finishes carry profilometer data, and how non-conformances are flagged rather than adjusted silently. A factory that names its instruments and its calibration is treating its measurement as evidence; one that answers vaguely is treating it as decoration, and on a tight-tolerance order, the decoration is exactly where the risk lives.
Agree the sampling plan with the same care, because a tolerance held on the first article is not a tolerance held through the run. Ask how often the critical features are measured during production, what happens when a sample drifts toward the band edge, and what the lot report will show — a factory that can state its sampling in numbers is running a controlled process, while one that cannot is asking you to trust a long run on a single first article. The capability table describes the process at its best; the sampling plan describes the process in operation, and the lot report is where the two meet.
How do material and geometry change what can be held?
The capability table is the floor, and the material and the geometry decide how hard each feature is to hold. Aluminum cuts fast and holds finishes easily, but it expands about twice as much as steel for a given temperature change, so a large aluminum part measured warm and cold can read differently, and thin walls move as stress is released. Stainless cuts slower, work-hardens in the cut, and traps heat, which makes a tight band on a thin stainless wall harder to hold than the same band in aluminum — the process strategy has to protect the edge and the dimension at once.
When a drawing couples a demanding geometry with a demanding material, the factory's review should say so, and the fix is usually a design adjustment or a fixture change rather than a tighter cut. A thin wall that holds its band easily in aluminum fights harder in stainless; a large flat face that stays flat in steel can bow in aluminum as residual stress releases. Both families are machined on this floor to the same stated capability, but the quote and the process discipline differ, and the DFM review is where that reality belongs — before the drawing is committed, not after the first article arrives.
How do you specify tolerances and finishes on a China order?
Everything above condenses into a specification discipline that travels with the RFQ.
- Call out the band on the functional features only. Tolerances and finishes belong on the surfaces that mate, seal, slide, or rotate; the rest rides on a general block.
- Separate size, geometric, and finish callouts. Diameters on the dimension lines, roundness and true position as geometric tolerances, Ra values on the surfaces that need them — each verified by its own instrument.
- Name the measurement reference and the instruments. State 20 °C for dimensional measurement and confirm the CMM and profilometer coverage for the critical features, so the report you receive is the report you can audit.
- Ask for capability evidence, not adjectives. A factory that states ±0.003 mm on milling and turning, ±0.002 mm on grinding, and Ppk ≥ 1.67 at the initial study on critical characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window is describing real work; one that says "high precision" is not.
Keep the closing rule in front of you: a drawing is a set of numbers the factory must hold and measure, and the buyer who specifies only what the function needs — and verifies what the factory claims it can hold — gets the part at the right price with the evidence to prove it. The capability is real, the callouts decide the cost, and the measurement decides whether the numbers on the drawing are the numbers in the part.
Frequently Asked Questions
What tolerances can a China machining factory actually hold?
Milling and turning hold ±0.003 mm on controlled features, and precision grinding reaches ±0.002 mm as a separate process family, with process capability Ppk ≥ 1.67 at the initial study on critical characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window. Geometric callouts such as true position, runout, and concentricity carry their own bands and need CMM-level verification.
What surface finishes can machining achieve?
Standard milled and turned finishes sit in the Ra 1.6–3.2 µm range; refined passes reach Ra 0.8 µm; and grinding, lapping, or polishing reaches Ra 0.4 µm and below as separate operations. Each step down the finish ladder adds process time and inspection cost.
How do I specify tolerances on a drawing for a China factory?
Call out the band on the features that mate, seal, slide, or rotate, and leave the rest on a general block. Name the geometric callouts separately — roundness, runout, true position — and agree the measurement reference of 20 °C, because the drawing is what the factory quotes against.
What is the difference between a dimensional tolerance and a surface finish callout?
A dimensional tolerance controls a size — a diameter, a length — while a finish callout controls the surface texture left by the process. They are independent: a diameter can be on nominal and still carry a rough finish, or a fine finish and sit out of band. Both need their own callouts and instruments.
What does Ppk ≥ 1.67 initial mean on a machining order?
It is the process capability target: the part distribution sits inside the tolerance band with enough margin that a stable run stays in specification, rather than hugging the edge. It is the statistical statement that a tight tolerance is being held by the process, not met by luck on the first article.
How is a tight tolerance or fine finish verified?
Dimensional features are measured on a CMM at the 20 °C reference, geometric callouts on the instruments that resolve them, and finishes with a surface profilometer. An instrument should resolve about ten times finer than the band it judges, so a ±0.003 mm feature belongs on a CMM, not a hand gauge.
Need a factory that will state its capability in numbers?
Send the drawing through the contact page — the review will come back with the tolerance and finish bands for each functional feature, the instruments that will verify them, and the process route behind the quote.